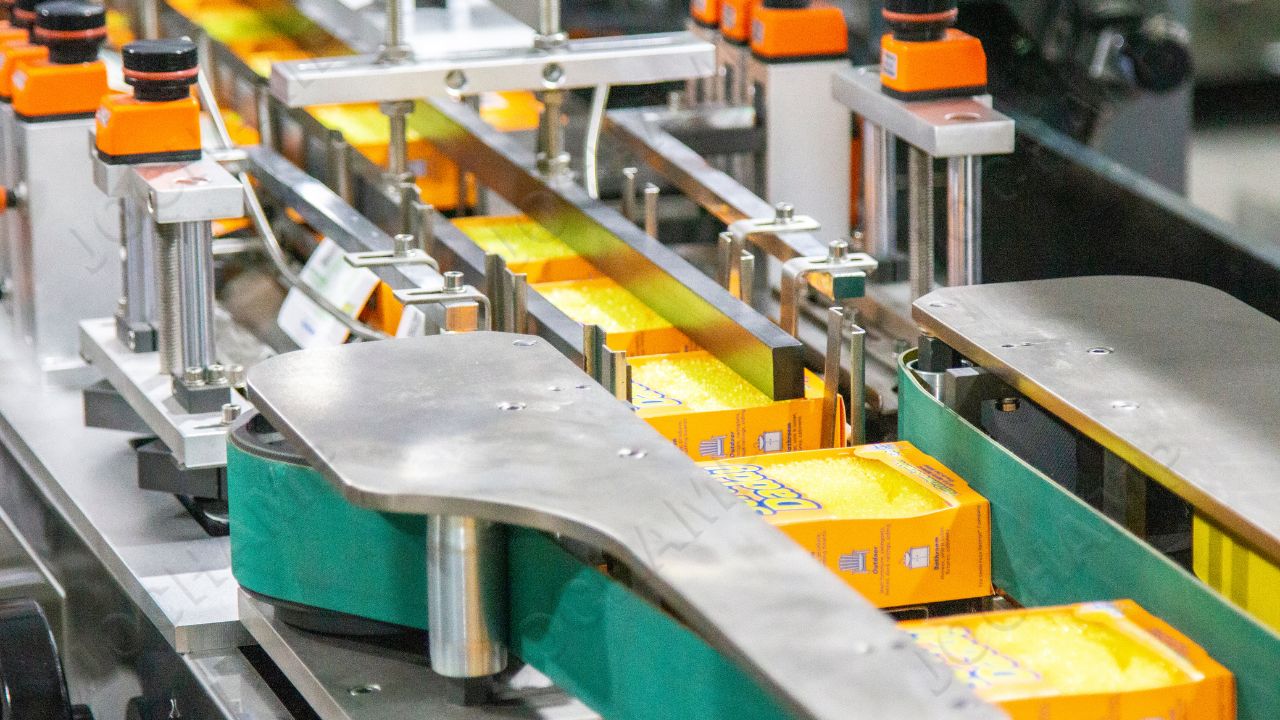
In modern food and beverage industries, cartoning machines are an integral part of efficient packaging. From cereal boxes to frozen meals, streamlining these processes helps businesses save time, reduce costs and ensure compliance with FDA standards.
Today, we will explore key uses of cartoning machines that will help your operations remain competitive in the dynamic market.
Product Protection and Preservation
· Physical Protection
Cartoning machines provide you with sturdy outer packaging that keep food products free from all mechanical damage as it goes through handling, transportation, and storage. Also, they prevent products from crushing, getting deformed, and breaking, ideally if the items you package are delicate such as baked goods or biscuits.
· Environmental Protection
Cartons serve as a barrier against all environmental factors like air, light, and moisture. This is critical if your factory is producing food products that are sensitive to oxidation or humidity. It helps to extend the shelf life of your products and maintains its freshness.
· Preventing Contamination
When you use cartoning machines to enclose food products properly, they help in reducing exposure to microbes, dust, and some other contaminants.
Remember, cartoners for food industry are CGMP compliance. By maintaining high hygiene standards, it implies that the machine is easy to clean, with parts that are in direct contact with the food having a surface roughness (Ra) of ≤ 0.8 µm.
Marketing and Branding
· Enhance Shelf Appeal
Cartons generally offer a printable surface where you can have high-quality graphics, branding elements, and product information pasted on it. Attractive packaging enhances visibility on retail shelves as well as influences consumer purchasing choices.
· Brand Differentiation
As part of the marketing strategy, you can create unique carton shapes that can help differentiate your products in the market. That is, you can create unique packaging that give your brand a unique identity.
So, the unique carton shapes, designs, and finishes aid in ensuring your brand stands out.
· Consumer Convenience
Cartons can be easily designed with user-friendly features like resealable flaps, easy-open tabs, and portion-friendly packaging. Therefore, your customers will have unique experience, which will motivate them to buy your products.
Operational Efficiency and Cost Reduction
· Automated Packaging
Cartoning machines ensures your entire packaging process is automated. This significantly cuts down manual labor.
These machine feature servo motor systems, PLC control systems and robotic arms that help improve efficiency. Additionally, automation guarantee accurate packaging and consistent output.
· Material Optimization
The high degree of accuracy reduced material wastage hence you will realize significant cost savings. They cut, form, fill and seal cartons with high degree of precision.
· Integration with other Systems
Cartoning machines can be easily integrated with other down and upstream equipment like labeling systems, filling machines, and palletizers. That is, after processing foods, they move straight to the cartoning section, which is part of the complete production line. This reduces possible downtime, or contamination that may occur when transporting food products to be packaged elsewhere.
Packaging Applications to Specific Products
· Dry Food Products
Food products like pasta, cereals, snacks, and rice are packaged mostly with cartoning machines. These cartons safeguard these products from physical and moisture damage even as it allows for easy stacking and storing.
· Confectionery and Bakery Items
Food items like cakes, chocolates, biscuits, and pastries are also major beneficiaries of cartoning. This is because they need to both be protected and require an attractive presentation. Cartons aid in maintaining freshness and shape of your food items or products even as it enhances its visual appeal.
· Refrigerated or Frozen Foods
Cartoning machines are perfect for packaging frozen meals, chilled, and ice cream products. If your products require cartons that can withstand low temperatures as well as prevent moisture loss or freezer burn, specialized cartons will make it happen.
· Beverage Packaging
All over the world, cartons are used for packaging beverages like milk, juices, as well as plant-based drinks. These cartons are designed mostly to have protective layers. Also, they are designed to provide you with easy storage and pouring features.
· Health and Nutritional Products
Cartoning machines can be used to carton-package products like meal replacements, protein bars, and supplements. These are done to ensure the right control of portions, safety, and branding consistency.
Regulatory Compliance
· Sustainable Packaging
Cartoning machines are designed to support the use of biodegradable and recyclable materials. You can use cartoners to achieve your sustainability goals by adopting eco-friendly materials.
· Compliance with Safety Packaging Standards
Cartoning machines are made to meet food safety standards or regulations. So, you can be assured that the machine you use meets hygiene standards, is tamper-evident packaging, and labeling requirements.
FAQs
1. What are the emerging trends in cartoning machines for food industry?
Some emerging trends include the integration of robotics, smart automation, sustainable packaging solutions, and IoT-enabled monitoring systems.
2. What types of food products are most commonly cartooned?
Food products that are most commonly cartooned are frozen meals, cereals, dairy products, snacks, health supplements, confectionery items, and beverages.
3. What is the difference between horizontal and vertical cartoners?
Horizontal cartoners where product loading is concerned load on the side (side loading), while vertical cartoners are top loading.
4. Differences in table format
| Feature | Horizontal Cartoners | Vertical Cartoners |
| Product loading mechanism | Loads from the side or horizontally | Loads from the top or vertically |
| Ideal products | Solid or pre-formed items like bars, trays, etc. | Loose or granular items like grains, powders, etc. |
| Speed | Quite higher | Moderate |
| Space requirement | Requires a larger footprint | Quite compact |
| Complexity | Highly complex | Simple design |
| Common uses | Frozen and confectionery foods | Cereals and dry foods |
5. How does cartoners ensure food safety and hygiene?
Since cartoning machines are designed with food-grade materials and a hygienic design, they are very easy to clean and maintain. This is what ensures food safety and hygiene.
6. How fast can food cartoning machines operate?
The speed of food cartoning machines vary depending on the type of machines and product. However, most fully automatic cartoners can handle from 30 to over 400 cartons per minute.
Partner with Neocarton
Neocarton is a leading cartoning machine manufacturer trusted by top food processing factories in the U.S.A., Europe and Asia. Our food cartoner are designed to comply with the CGMP requirements with parts that are in direct contact with food made from stainless steel – Request for a quote today.